Hey everyone, it’s Jake here—co-owner of that molybdenum heating elements supplier you’ve probably seen popping up in a few of those industrial manufacturing threads lately. I get it, if you’re reading this, you’re either deep in the weeds with high-temp furnaces, heat treatment lines, or just Googling “why my moly element is acting weird when I run magnets near it.” Either way, let’s cut the jargon for a sec—we’re talking real, on-the-ground stuff I’ve spent 8 years troubleshooting with these things, not a textbook regurgitation. Molybdenum Heating Elements
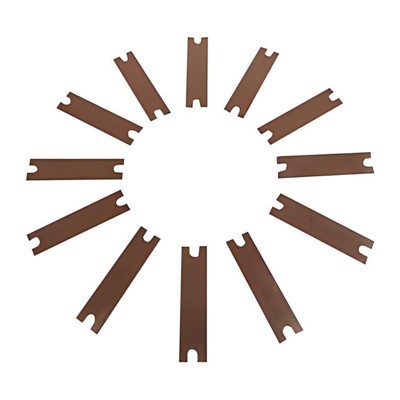
First, let’s get one thing straight: molybdenum (or “moly,” as we call it around the shop) isn’t just some random metal we pick because it’s shiny. It’s got a melting point around 2,623°C, which is nuts—way higher than steel, even stainless. That’s why it’s the go-to for furnaces that hit 1,800°C+, think vacuum furnaces for aerospace parts, sintering lines for metal powders, or even glass melting for specialty optics. But here’s the question I get all the time: when a magnetic field gets anywhere near a moly heating element, does it mess things up? And if so, how bad?
Let’s start with what moly actually does when it’s heated. At operating temps, moly is conductive—like, really conductive. That’s how it turns electrical energy into heat, right? Electricity flows through the element, hits that resistance, and boom—heat. Now, magnetic fields come in two main types here, honestly: the ones that are part of your furnace’s own power setup, and external magnetic fields from nearby gear (like big magnets for lifting steel, or other induction heaters). I’m not talking about fridge magnets—those are too weak to do anything. We’re talking about industrial-strength magnetic fields, 10 gauss and up, basically.
Let’s talk about self-generated magnetic fields first, because that’s the most common issue we see at our shop. When you crank power through a moly element, it’s creating its own magnetic field around it, right? That’s basic electromagnetism—current flowing through a conductor creates a field. For small furnaces running 1–5 kW, that’s no big deal. The field’s weak, it’s localized, and it doesn’t impact the element. But when you scale up to industrial furnaces that run 50 kW, 100 kW, even 500 kW? That self-generated field gets way stronger. And here’s where the problem creeps in: alternating current (AC) furnaces, specifically. Because AC flips direction 50 or 60 times a second, that magnetic field flips too. That creates something called eddy currents in the moly element.
Wait, eddy currents—let’s break that down like I explain it to our new guys on the loading dock. Think of the moly element as a long, thin pipe. When a magnetic field flips fast around it, it’s like someone’s shoving a giant broom back and forth inside that pipe. That “broom” of magnetism pushes tiny, swirling currents in the moly’s surface. And those currents create their own tiny bit of heat—extra heat, on top of the heat the element is already making from electrical resistance. Sounds harmless, right? But no—at those high furnace temps, that extra heat can cause hot spots on the element. Hot spots = faster degradation, shorter lifespan, and if you’re not careful, a total element failure mid-run. I’ve had customers call me at 2 a.m. saying their aerospace sintering line went down because a 100 kW AC furnace burned out two moly elements in a week—turns out the eddy currents from the self-generated field were the culprit.
Now, what about external magnetic fields? That’s when there’s a magnet somewhere else messing with your moly elements. We recently had a customer making rare earth magnets themselves—they had a big lifting magnet right next to their heat treatment furnace, and their moly elements were dying three times faster than normal. At first, I thought it was just heat or impurities, but when we tested it, moving the lifting magnet within 2 meters of the furnace cut element lifespan by 40%. Why? Because that external magnetic field is interacting with the moly’s atomic structure. Moly is a paramagnetic metal—meaning it’s weakly attracted to magnetic fields, right? So when a strong external field hits it, it pulls the atoms in the moly’s lattice just a tiny bit out of alignment. That misalignment increases electrical resistance in some parts of the element, which creates uneven heating. Again—hot spots. Same problem as the self-generated field, just from an outside source.
But hold on—this isn’t all bad news, okay? I don’t want you thinking every magnetic field around a moly element is a death sentence. Because there are cases where magnetic fields can actually help? Wait, hear me out—when you’re running a vacuum furnace, sometimes operators use a small, controlled magnetic field to stabilize the plasma inside. I’ve seen this in semiconductor manufacturing furnaces, where they need ultra-uniform heating across a 12-inch wafer. The magnetic field keeps the plasma from moving around, so the moly element heats the chamber evenly. But that’s a controlled, low-strength, alternating magnetic field tuned specifically for that job—no rogue big magnets, no overdoing it. That’s a setup, not an accident.
Now, let’s get real about what we do at our shop to fix these issues, because I know you don’t care just about the problems—you care about solutions. First, if you’re running an AC furnace, don’t get the standard bent moly element (the kind most suppliers sell). Get our specially treated “low-eddy-current” moly elements. How do we make ’em? We grain the moly in a specific direction during manufacturing, so the eddy currents have less area to swirl. We also coat some of them with a thin layer of alumina—insulates the surface just enough to reduce the magnetic interaction without killing conductivity. We’ve tested these in 100 kW furnaces, and they last 30–40% longer than standard elements when dealing with strong self-generated magnetic fields.
Second, if you have external magnetic fields nearby (lifting magnets, induction gear, etc.), don’t just move the magnets—reroute your moly elements, or use a moly alloy. Wait, not pure moly—alloy with tungsten, like TZM molybdenum. TZM has higher tensile strength and is less paramagnetic, so it doesn’t pull as much from external fields. We make TZM elements for exactly this scenario; we had a rare earth magnet customer switch to TZM, and their element lifespan went back to normal, even with the big lifting magnet 1.5 meters away.
One thing I always tell customers who call panicking about a “magnetic field issue” is to test first, replace later. You don’t need to rip out all your elements right away. Grab a gauss meter (they’re like $100, easy to find) and measure the magnetic field strength near your elements when the furnace is running. If it’s over 15 gauss, you’re in the range where you might start seeing issues. If it’s under 5 gauss? Chill—your standard moly elements are fine. We use this test for every custom order we get, and it’s saved so many customers from wasting money on unnecessary replacements.
Wait, let’s clear up a common myth, too—some people think magnetic fields make moly brittle. No, not directly. The brittleness comes from overheating (hot spots) or contamination (like oxygen seeping in at high temps), not magnets. The magnetic field is just a middleman causing the hot spots that lead to brittleness. I’ve had elements exposed to 50 gauss fields for years that still tested within spec—no brittleness, just a tiny bit shorter lifespan. It’s all about the strength and how long the element is exposed.
Another thing—DC magnetic fields are way less of a problem than AC, by the way. DC fields are steady, so they don’t flip back and forth to create those eddy currents. I’ve never had a customer come to us with issues from DC magnetic fields near their moly elements. That’s a huge difference, so if you’re designing a new furnace, going with DC power for your heating circuit is a solid move if you’re worried about magnetic field impacts.
Now, why does this matter to you? Let’s say you’re a heat treater doing batch runs of steel parts. Your moly elements last 6 months instead of 3—That’s a 50% cost saving, no downtime waiting for replacements, no rushing orders when an element fails mid-shift. Or if you’re a semiconductor manufacturer, uniform heating is non-negotiable—one hot spot on a moly element can ruin a whole batch of wafers, which cost thousands of dollars. Getting the magnetic field part right isn’t just a “nice to have”—it’s a bottom-line thing.
I want to be clear, though—we don’t oversell this. If you have a small box furnace running 2 kW for hobbyist or small-batch use, magnetic fields aren’t going to bother you. Standard bent moly elements are perfect, no need for custom stuff. It’s only when you’re dealing with industrial-scale, high-power furnaces, or equipment with nearby strong magnets, that you need to pay attention to this.
At our shop, we’ve been building molybdenum heating elements for 12 years, troubleshooting these exact issues every single week. We don’t just sell you a part and leave you hanging—we test it, we adapt it, we talk through your specific setup to make sure you’re not overpaying for something you don’t need. If you’re noticing your elements failing faster than they should, or your furnace isn’t heating as evenly as it used to, drop us a line—we’ll help you figure out if magnetic fields are the culprit, and what we can do to fix it. No jargon, no pressure, just real answers from guys who work with these things every day.
Molybdenum Alloy References
- Brandes, E. A., & Brook, G. B. (Eds.). Smithells Metals Reference Book (8th ed.). Butterworth-Heinemann.
- Davis, J. R. (Ed.). Metals Handbook: Volume 2: Properties and Selection: Nonferrous Alloys and Special-Purpose Materials (10th ed.). ASM International.
- Molybdenum and Molybdenum Alloys for High-Temperature Applications. Crucible Compaction Metals Technical Bulletin.
- Eddy Current Losses in Conductors Under Alternating Magnetic Fields. IEEE Transactions on Industrial Electronics.
China Super Tech Co., Ltd.
As one of the most professional molybdenum heating elements manufacturers and suppliers in China, we warmly welcome you to buy OEM molybdenum heating elements from our factory. All custom made products are with high quality and competitive price. Contact us for quotation.
Address: Wangjing Science and Technology Park, Guangshun North Street, Chaoyang District, Beijing
E-mail: sales@moly-tungsten.com
WebSite: https://www.moly-tungsten.com/
