Hey everyone, I’m Jake—been running the sales side of our round packaging box forming machine business for over 8 years, and let me tell you, one of the most common questions I get from new clients is: “How the heck do I adjust the material tension on this thing without messing up a whole run?” For anyone who’s worked with these machines, you know tension’s make-or-break. Too loose, and your circular boxes come out wrinkled, lopsided, or with that annoying wavy edge on the bottom. Too tight, and you’ll snap the material mid-form, stretch the cardboard or plastic so bad it loses its shape, or even wear out the feed rollers way faster than they should. I’ve seen this trip up small packaging startups and big-name brand teams alike, so today I’m walking you through exactly how to dial that tension in right—no fancy engineering degree required. Round Packaging Box Forming Machine
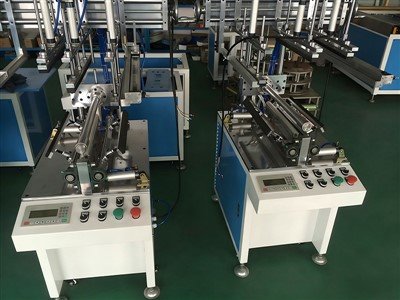
First, let’s keep this real: I don’t care how fancy your machine’s control panel is, or how much you paid for it. Tension adjustment boils down to watching how the material moves through every single station, from the unroll stand all the way to the forming die. Skip this step, and you’ll be stuck reworking boxes until you’re ready to throw your tablet across the workshop. Let’s start with the basics you can’t skip before even touching any knobs: pre-run checks. I get it, everyone’s in a hurry to start a 10,000-piece run, but take 2 minutes first. Make sure your material roll is loaded straight on the unroll mandrel—no side-to-side wobble there. If it’s crooked, the tension will be uneven on left and right, and you’ll have bad boxes on one side before you even begin. Next, pull 2-3 feet of material out, run it through the feed rollers, past the guide rollers, and to the forming station, then cut it. This “test length” is your window to see what’s actually happening without wasting a whole box blank.
Now, let’s break down the key tension zones on a typical round forming machine, because adjusting the whole machine at once never works. Most machines have three main tension spots: the unroll stand, the intermediate guide section (between unroll and forming die), and the feed rollers right before the die. Each of these does a specific job, so you tweak them one at a time, in order. Let’s start with the unroll stand. This is what keeps the material from just peeling off the roll too fast when the feed pulls it. If your unroll tension is too low, the roll will spin freely, and the material will bunch up before the next set of rollers. Too high, and you’re putting unnecessary stress on the roll core, which can crack, or you’ll drag the material so much it stretches before it even gets to the forming step. How do I adjust this? Almost all unroll stands have a pneumatic brake or a simple torque adjustment knob. For cardboard materials (super common for food boxes, cosmetic containers), I set the unroll tension so that when you pull the test material by hand, it takes about 10-15 lbs of force to pull steadily—test that with a cheap luggage scale, no fancy tools needed. For thicker plastic film used for rigid packaging, bump that up to 15-20 lbs, since plastic’s more slippery and prone to sliding on the roll if tension’s too low.
Next up, the intermediate section—this is the part between the unroll and the forming die, which most people skip, but it’s the secret to consistent tension. Here, you’ll have a set of idler rollers, sometimes a dancer arm, that keeps the material moving smoothly between stations without slacking. A dancer arm is super common on mid-range to high-end machines like ours, and it’s there for a reason. If the dancer arm’s all the way up, that means tension is too low—material’s bunching up here. If it’s all the way down, tension’s too high, and you’re pinching the material between the guide rollers and stretching it. The sweet spot is when the dancer arm sits dead center, moving slightly as the machine runs, not stuck at either end. If you don’t have a dancer arm (some entry-level machines skip this), you’ll adjust a set of guide rollers that can be tensioned with small spring screws. Turn each screw a quarter turn at a time, run a short test, and check that the material isn’t slipping on the guides or buckling in this section. I can’t tell you how many clients call me saying their boxes are wrinkled, and it’s because they messed up this intermediate tension zone, not the feed.
The last and most critical zone is the feed rollers right before the forming die. This is where the final tension is set, because this is what’s feeding the exact length of material needed for each round box blank. Too much tension here, and you’ll get a stretched blank that when formed, has a gap in the seam, or a bottom that’s too small. Too little, and the feed rollers will slip, pulling uneven lengths, so your boxes will have mismatched heights. How to dial this? First, make sure your feed rollers are clean—oil, cardboard dust, or plastic residue makes them slip, no matter how much tension you set. Wipe them down with isopropyl alcohol before every run, trust me. Then, adjust the tension on the feed rollers: most have a pressure adjustment lever on the roller assembly. For cardboard, you want the rollers tight enough that when you try to slip the test material out from between them, you have to tug hard, but not so tight that you dent the cardboard. For rigid plastic, they need to be a little snugger, since plastic is less grippy. Run that test length again, and check the length of the blank: if it’s too short, the feed is pulling too much tension (slipping would make it longer, wait no—hold on, let’s get that right. If tension’s too high on the feed, it stretches the material, so the blank you get when the cutter triggers is shorter than it should be. If tension’s too low, the rollers slip, so the blank is longer. That’s a quick way to diagnose.
Wait, I should add a quick troubleshooting step for common mistakes I see all the time. Let’s say you adjust all that, run a test box, and the bottom is wrinkled. What gives? 9 times out of 10, it’s uneven tension across the width of the material. That’s usually because the guide rollers aren’t aligned straight, or one side of the unroll stand’s brake is set differently than the other. So take 30 seconds to check that all guide rollers are parallel to the forming die, not tilted to one side. Another common one: tension changes when you switch between materials. If you’re going from 12pt cardboard to 16pt, or from cardboard to PET plastic, you can’t just keep the same tension settings. Thicker, stiffer materials need higher tension to keep them straight through the forming step, while thinner, more flexible stuff needs lower tension so it doesn’t crumple. I always tell clients to create a quick cheat sheet for their common materials—write down unroll tension, intermediate dancer position, and feed roller pressure for each, so they don’t have to re-adjust from scratch every time they switch.
Also, a pro tip from our service team: if you’re running a long run (like 50,000+ boxes), check the tension halfway through. Things change as the roll gets smaller—when the roll’s half gone, the unroll tension will feel different because the circumference is smaller, so it spins faster. So stop at 25k pieces, run a test blank, and tweak the unroll tension just a tiny bit, like a quarter turn on the brake knob. That small adjustment will save you from a whole batch of garbage boxes at the end of the run.
Now, let’s talk about our machines specifically, since a lot of you reading this are running our round packaging box formers. We built our machines with that exact adjustment process in mind—no confusing menus, all physical controls that are easy to reach, and we include a quick start guide with specific tension ranges for every material we’ve tested. If you’re using a different brand, some of this might be a little different, but the core logic is the same: adjust each zone in order, test, tweak, don’t guess.
I get that working with industrial equipment can be frustrating, especially when you’re on a tight deadline. The last thing you need is to spend 2 hours troubleshooting tension when you could be hitting that production target. If you’re dealing with persistent tension issues, or you’re looking to upgrade a machine that’s giving you headaches, our team is here to help. We’ve helped hundreds of packaging operations—from small startups just getting off the ground to large consumer brands—optimize their tension settings, reduce downtime, and cut down on waste. No sales pitch, just real advice from people who work with these machines every single day.
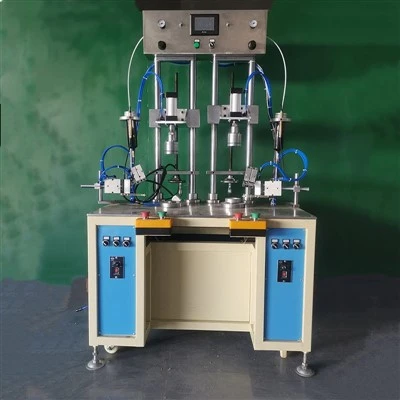
PVC Cylinder Edge Curling Side Machine If you want to chat about your specific setup, need a custom cheat sheet for the materials you use, or even if you just have a quick question, reach out anytime. We’re always happy to help fellow packaging folks solve problems and keep production running smooth.
References
- Industrial Packaging Machinery Association. (2021). Operational Best Practices for Circular Box Forming Equipment.
- Smith, L. (2019). Tension Control for Flexible Packaging and Rigid Forming Machines. Packaging Engineering Journal.
- Technical Services Team, [Our Round Packaging Box Forming Machine Supplier]. (2023). Field Adjustment Guide for Standard Round Forming Lines.
Titagong (Dongguan) Machinery Co., Ltd.
We are one of the most reliable manufacturers and suppliers of round packaging box forming machine in China. With abundant experience, we warmly welcome you to buy bulk high quality equipment in stock here and get pricelist from our factory. For price consultation, contact us.
Address: No.149, Qingyi Road, Qingxi Town, Dongguan City, Guangdong Province, China
E-mail: shuaizoe@gmali.com
WebSite: https://www.titagonggroup.com/
